
Pattern and mould preparation
The pattern and parting arrangement are reviewed from the drawing, sample or reference part. Moulding sand is prepared and compacted around the pattern to create the casting cavity.
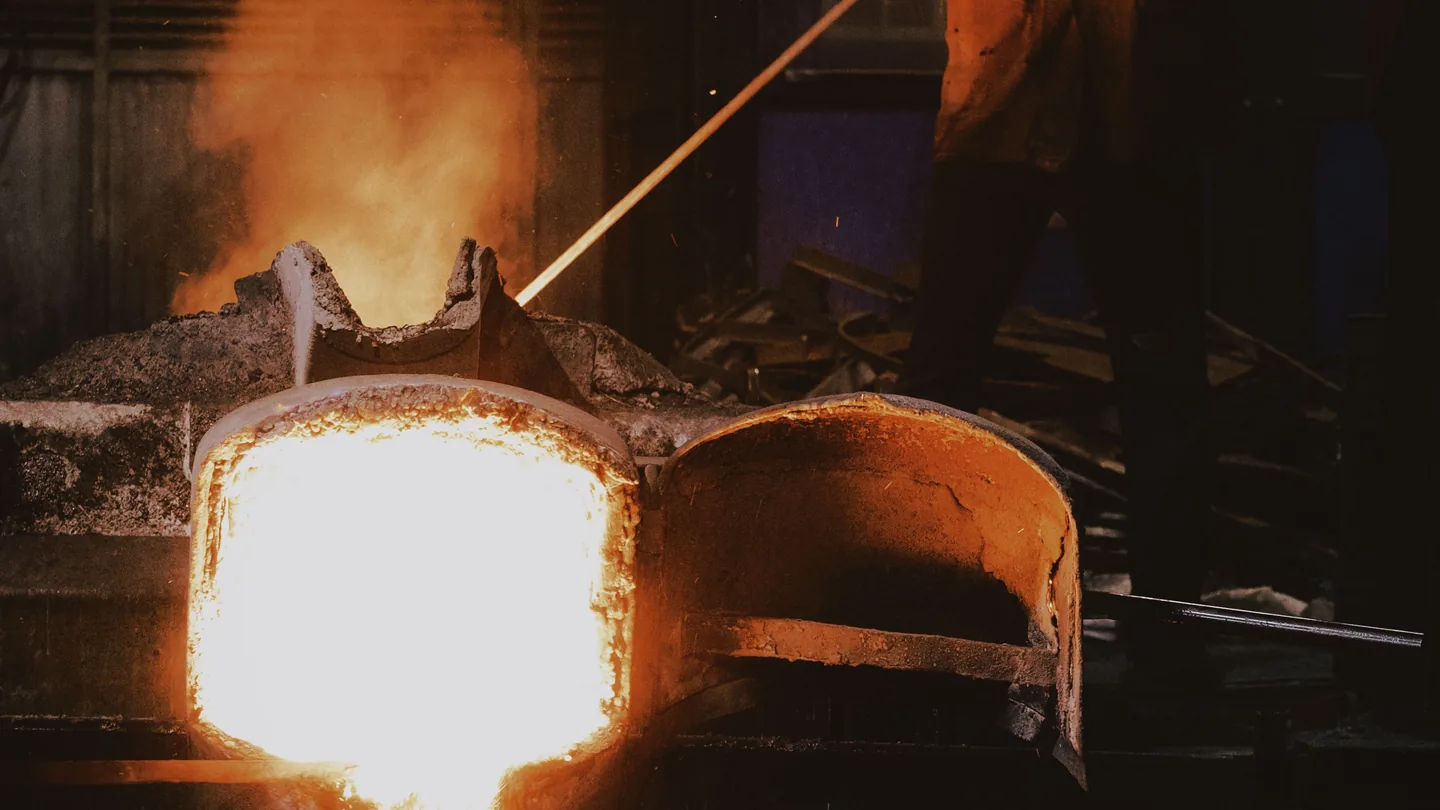
Гибкий и экономичный маршрут для средних и очень крупных отливок, включая детали дробилок, корпуса, рамы и индивидуальные компоненты.
Green sand casting uses compacted moulding sand around a pattern to form the cavity for the casting. It remains the practical workhorse for large and heavy components because the method supports a broad size range, a wide material family and relatively fast pattern preparation. The final route is selected against the drawing, part weight, geometry, material and working conditions rather than by size alone.
The exact controls, material grade and acceptance documents are confirmed against the part requirement.
The pattern and parting arrangement are reviewed from the drawing, sample or reference part. Moulding sand is prepared and compacted around the pattern to create the casting cavity.
Cores, runners, risers and the gating layout are arranged to support filling, feeding and the required geometry. Critical sections are reviewed before the mould is closed.
The selected alloy family is melted and poured into the prepared mould under the agreed process controls. Material and heat information can be recorded for the project file.
After solidification, the mould is broken down and the casting is separated from the sand. Runners, risers and excess material are removed for the next stage.
The casting moves through the agreed heat treatment, fettling, machining and inspection scope. Dimensional, hardness, visual or additional checks are defined before production.
Green sand castings are commonly followed by heat treatment, shot blasting or fettling, machining on critical interfaces, dimensional inspection and export packing. The exact sequence is fixed during technical review so the casting, hardness and machined features match the buyer's acceptance requirements.